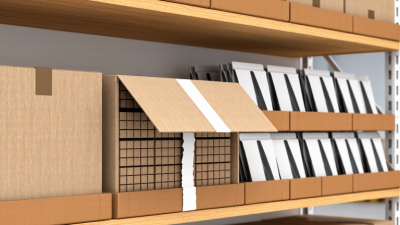
Choosing the best shelf ready packaging is not simply a matter of adding bright graphics to a shipping carton. It must protect products in transit, open cleanly in store, and display items clearly on a crowded shelf. A good choice depends on the product’s weight, shape, fragility, and replenishment needs. For example, a heavy jar may need a stronger base, while a lightweight snack pouch may benefit from a compact tray that keeps facings neat. Small details matter.
Retailer requirements also shape the decision. Check case dimensions, shelf space, preferred opening methods, and how staff will move the pack from pallet to display. Perforations should tear predictably without damaging products, and printed information should remain visible after the front panel is removed. Material choice matters too: board strength, moisture exposure, and stacking conditions can affect performance. There is no universally best format. A design that looks impressive in a mock-up may be awkward to open or too large for the shelf. Even experienced teams can miss this. Testing filled packs through shipping, handling, and in-store setup can reveal problems before a wider rollout. This guide explains the practical criteria to compare, the questions to ask suppliers, and the trade-offs worth reviewing before making a decision.
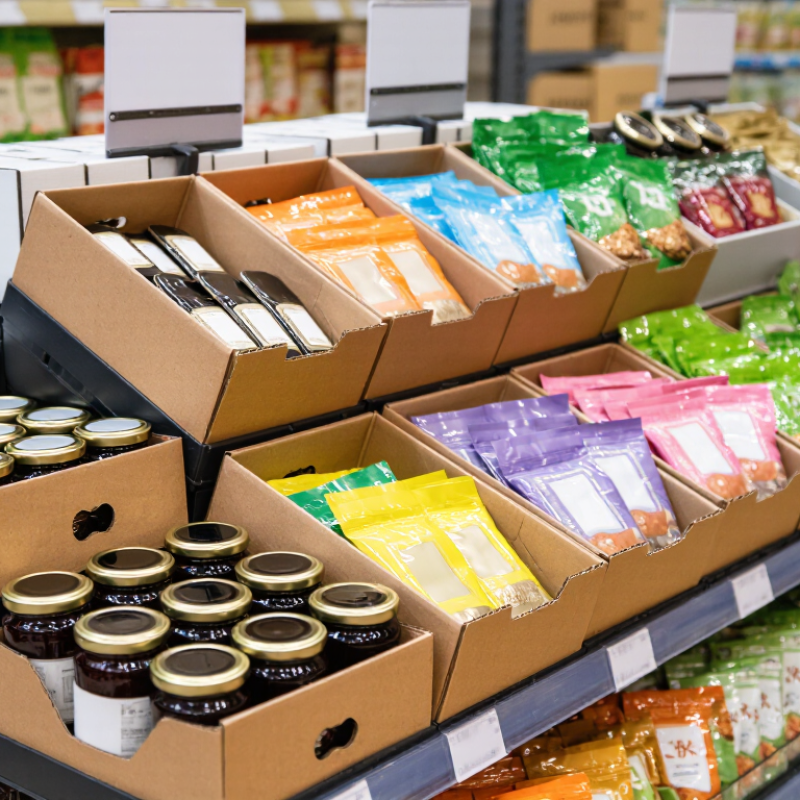
Choosing shelf-ready packaging starts with the retailer’s real operating conditions, not a preferred carton style. Check shelf depth, height, loading direction, and required facings. Measure the actual shelf. Confirm whether staff need to open the case quickly, place it without removing products, and keep the front panel visible. A tear strip that works on a packing line may still be awkward in a busy aisle. Then test it.
SKU details shape the format. Record each item’s dimensions, weight, packaging strength, and sales rate. A shallow tray may suit light, stable products, while heavier items may need stronger walls or a different case count. Mixed variants can complicate identification and restocking, so labels and product orientation matter. Do not rely only on outer measurements; items can shift during shipping and leave gaps on shelf.
Shelf requirements include more than fit. Check how many facings are available, how neighboring products affect access, and whether staff can replenish the unit safely. A small store trial can reveal crushed corners, blocked labels, or a tray that takes too long to load. These details are easy to miss in a drawing. Adjust the format after observing actual handling, even when the first sample looks neat.
| Product / SKU Profile | Retailer and Shelf Requirements to Define | SRP Format to Consider | Why It May Fit | Checks Before Approval |
|---|---|---|---|---|
| Small, lightweight cartons Example: individually boxed household or personal-care items; several facings per shelf. |
Confirm shelf width and depth, target facings, replenishment method, and whether staff need to load products from the front. | Perforated corrugated tray with a removable front panel. | Keeps units grouped during transport while allowing the front to be opened for shelf presentation. | Check that the tray fits the shelf footprint, the tear line opens cleanly, and the remaining tray is stable when partly empty. |
| Flexible pouches Example: lightweight refill or snack pouches that can slump when unsupported. |
Establish shelf depth, required product orientation, number of units per facing, and whether the retailer uses shelf dividers. | Corrugated tray with a higher back and low front wall; consider a divider for multiple variants. | Provides support for flexible packs and helps keep product fronts visible after opening. | Test pack stability, label visibility, access to the back row, and whether the front wall hides product information. |
| Bottles or other upright containers Example: rigid containers that may tip during handling or shelf replenishment. |
Confirm container diameter, shelf depth, number of facings, product weight, and whether the shelf has a retaining lip. | Corrugated tray with a reinforced base and suitably low front wall; use cells only where separation is needed. | Supports the product group and can reduce movement while avoiding unnecessary individual compartments. | Check base strength under load, bottle-to-tray clearance, tipping resistance, and whether the tray can be lifted safely when full. |
| Heavy or dense multipacks Example: canned or boxed goods sold in compact shelf quantities. |
Define the maximum shelf load, replenishment quantity, handling route, and whether the retailer permits direct placement from a shipping case. | Reinforced corrugated tray or a case-convertible design with a controlled tear-away opening. | A reinforced structure can support heavier contents; a case-convertible format may reduce handling steps when accepted by the retailer. | Validate compression and handling performance with the actual packed product; confirm opening instructions and shelf-load limits with the retailer. |
| Multiple flavors, sizes, or variants Example: a product family stocked together but requiring clear separation. |
Determine whether variants share a shelf section, need separate facings, or must be replenished as distinct SKUs. | Multi-compartment tray or separate single-SKU trays, depending on the retailer's planogram and replenishment rules. | Separators can help maintain variant organization; separate trays can simplify replenishment when each SKU is managed independently. | Verify SKU identification, compartment fit, barcode accessibility, and that mixed-SKU packing is allowed. |
| Limited shelf space or frequent replenishment Example: compact items with high sales velocity or narrow shelf allocation. |
Measure the usable shelf footprint, establish the target stock quantity, and review how quickly staff can remove, open, and replenish the pack. | Compact, easy-open tray sized to the agreed shelf footprint; consider a case-ready format if retailer procedures support it. | A footprint matched to the shelf can reduce wasted space and make replenishment more straightforward. | Conduct a shelf-fit trial, check access to every unit, and time the opening and replenishment process with store staff. |
Planning note: Shelf dimensions, allowable loads, opening methods, and case-pack rules vary by retailer and store fixture. Confirm the current requirements with the retailer and validate the selected SRP using the actual product, packed case, and shelf before production.